If you’ve ever driven past a tanker truck marked with bright cryogenic warning symbols, or stood near a well-insulated storage tank at a processing plant, you’ve probably wondered how that massive piece of equipment keeps liquefied gases stable, safe, and operational around the clock. As someone who’s spent the last 12 years designing, building, and troubleshooting liquefaction storage equipment for industries ranging from industrial gas production to renewable energy, I can tell you there’s a lot more going on behind those insulated walls than just holding cold liquid. The control systems that run these units aren’t just buttons and screens—they’re the backbone that prevents catastrophes, cuts operational costs, and keeps processes running smoothly, even in the harshest conditions. Today, I want to walk you through the core control systems that make modern liquefaction storage equipment work, from the ones that keep temperature and pressure in check to the ones that alert operators to issues before they become problems. Liquefaction Storage Equipment

Let’s start with the most fundamental of all: pressure control systems. Liquefied gases—whether it’s liquid nitrogen, liquid oxygen, liquid natural gas (LNG), or liquid carbon dioxide—are stored at very specific pressures, and even tiny deviations can have big consequences. For example, LNG stored at atmospheric pressure boils at around -162°C, so if the pressure inside the tank drops even slightly, the liquid warms up and vaporizes rapidly, which can cause pressure fluctuations that strain the tank’s structure. That’s why nearly every liquefaction storage tank relies on two layers of pressure control: primary and secondary. Primary pressure control systems use precision pressure transducers mounted directly on the tank’s vapor space to measure real-time pressure. If the pressure rises above a pre-set threshold, the system triggers two actions at once: it opens a vapor vent valve to release excess gas safely (directing it to a flare or recovery unit, depending on the gas) and signals a cryogenic pump to pull liquid from the tank and send it to another processing unit, which reduces the volume of liquid and lowers vapor generation. If pressure drops too low, the system activates a nitrogen or argon gas feed to repressurize the tank, ensuring it stays within its designed operating range. I still remember a project early in my career where a plant’s outdated pressure control system failed to catch a slow leak in a vent line, leading to a pressure spike that damaged a fraction of the tank’s insulation. That’s why modern pressure control systems aren’t just set-it-and-forget-it components—they have built-in diagnostic checks that test the transducers and valves daily, so operators get alerts if any part of the system is malfunctioning before a pressure event occurs.
Next up is temperature control, which is equally critical for liquefaction storage. Cryogenic liquefaction storage equipment has a multi-layered insulation system—usually made of vacuum panels, perlite, or polyurethane foam—that keeps the liquid cold, but no insulation is 100% perfect. Ambient heat seeps in over time, which causes the liquid to vaporize, a process called “boil-off.” For small, portable storage units, boil-off is manageable, but for large, high-capacity tanks used in industrial settings, even a 0.5°C temperature rise can lead to thousands of liters of vapor lost every day, wasting product and costing operators thousands of dollars annually. Temperature control systems are designed to counter this by monitoring the temperature of the tank’s inner wall, the insulation layers, and the vapor space, then adjusting the feed of refrigerated gas or recirculating existing boil-off gas through the tank’s cooling coils to maintain a consistent temperature. Some of our clients in food and beverage processing, which use liquid carbon dioxide to freeze and package products, require temperature stability within 0.1°C to ensure their CO2 stays pure, and our temperature control systems can deliver that level of precision. The best part about these systems is that they’re integrated with pressure control, so if a small amount of boil-off is detected, the system doesn’t just vent it—it sends it back through a liquefaction unit to be recondensed into liquid, eliminating waste and saving clients the cost of replacing lost product.
Beyond pressure and temperature, there are level control systems that keep operators informed about how much liquid is inside the tank at any given time. For storage equipment, getting an accurate level reading isn’t as simple as reading a fuel gauge in a car—cryogenic liquids are at extreme temperatures, so traditional float gauges can freeze or be damaged, and pressure fluctuations can skew readings. That’s why we use two types of level control systems in our equipment: ultrasonic level sensors and radar level transmitters. Ultrasonic sensors work by emitting high-frequency sound waves that bounce off the surface of the liquid, and the time it takes for the wave to return gives an accurate measurement of the liquid level. Radar transmitters use microwave signals, which are even more reliable in high-pressure, high-humidity environments, and don’t get affected by temperature swings. These level systems are integrated with the plant’s inventory management software, so operators can check the tank’s level from a remote screen, set low-level and high-level alarms, and even automate the process of refilling the tank when it gets too empty. I worked with a medical gas supplier a few years ago who was manually checking tank levels every day, a process that took their operators three hours per shift and sometimes led to stockouts when they miscalculated demand. After we installed our integrated level control system, their inventory management became fully automated, cutting operational time by 70% and eliminating stockout incidents.
Now, let’s talk about safety control systems, which are non-negotiable for liquefaction storage equipment, given the hazards of cryogenic liquids and flammable gases like LNG. These systems are designed to activate automatically if there’s an emergency, even if no operator is present, to prevent harm to people, equipment, and the environment. One of the most important safety systems is the emergency pressure relief system, which is separate from the primary pressure control system. This system includes large relief valves that are set to open at a pressure 20% above the tank’s maximum operating pressure, creating a failsafe if the primary control system fails. If a fire were to break out near the tank, the heat would cause the liquid inside to vaporize extremely quickly, and the emergency relief valve would discharge the excess vapor to a safe location, preventing the tank from rupturing. We also install gas detection systems that monitor for leaks of cryogenic gases or flammable vapors around the tank’s surroundings. These detectors are calibrated to trigger an alarm at 10% of the lower explosive limit (LEL) for flammable gases like LNG, and at 200 parts per million for toxic gases like carbon monoxide, giving operators time to evacuate and respond before a hazard becomes critical. Another key safety feature is the overfill prevention system, which is designed to shut off the liquid feed valve if the tank reaches 95% of its maximum capacity, preventing overflow. Overflow is one of the most common causes of storage incidents, as cryogenic liquids can severely damage equipment, and flammable vapors from overflow can ignite easily, so we build overfill prevention into every system we supply, with redundant sensors to make sure it works even if one component fails.
Finally, modern liquefaction storage equipment relies on data acquisition and remote monitoring systems, which have revolutionized how operators manage these units. Ten years ago, operators would have to be on-site 24/7 to check gauges, record readings, and respond to alarms, but today’s systems connect to the cloud, so data from pressure, temperature, level, and safety sensors is sent to a secure dashboard that can be accessed from a phone, tablet, or computer anywhere in the world. This remote monitoring allows our clients to track their equipment’s performance in real time, spot trends before they lead to problems, and even receive predictive maintenance alerts. For example, if a pressure transducer’s readings start to drift slowly over time, the system will flag this as a potential issue, so an technician can come to calibrate it during a scheduled shutdown, rather than waiting for it to fail and cause a pressure spike. We also provide customized reports for our clients that show boil-off rates, energy usage, and operational efficiency, which helps them optimize their processes and reduce costs. One of our renewable energy clients that stores liquefied biogas told us that since we installed our remote monitoring system, they’ve reduced their operational costs by 15% by cutting unnecessary maintenance and reducing waste from boil-off gas.
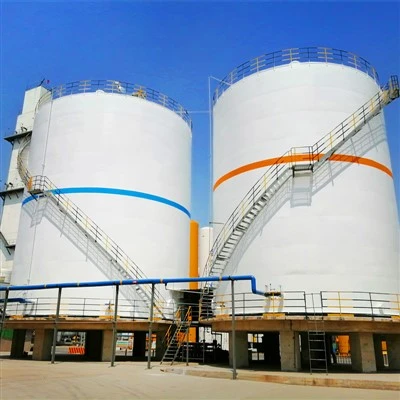
As a liquefaction storage equipment supplier, I’ve spent thousands of hours refining these control systems to meet the unique needs of each client. Whether you’re storing small quantities of liquid nitrogen for a lab or large volumes of LNG for a energy plant, the control systems have to be reliable, precise, and easy to use—because the last thing any operator needs is downtime or a safety issue. If you’re in the market for liquefaction storage equipment and want to learn more about how our control systems can improve your operations, or if you have questions about pressure, temperature, level, or safety controls for your existing equipment, we’re here to help. We work with clients across industries to design, install, and maintain customized solutions that fit their specific needs, and our team has decades of experience troubleshooting even the most complex storage challenges. Reach out to our team to discuss your requirements, and we’ll help you find the right control systems to keep your liquefaction storage equipment running safely and efficiently.
Type Of Air Separation Unit References
Cryogenic Storage Tanks and Their Control Systems. Cryogenic Society of America, 2021.
Liquefied Natural Gas Storage: Pressure and Temperature Management. International Gas Union, 2022.
Safety Standards for Cryogenic Storage Equipment. Occupational Safety and Health Administration (OSHA), 2020.
Automated Level and Pressure Control for Industrial Gas Storage. Industrial Gas Association, 2023.
Xinxiang Jiale Intelligent Equipment Co., Ltd.
As one of the most professional liquefaction storage equipment manufacturers and suppliers in China, we’re featured by quality products and good service. Please rest assured to buy durable liquefaction storage equipment for sale here from our factory. We also accept customized orders.
Address: No.3913, 9th Floor, Unit 3, East Commercial and Office Complex, Baolong City Plaza, Hongqi District, Xinxiang City, Henan Province, China
E-mail: cc2397410@gmail.com
WebSite: https://www.jiale-asu.com/
